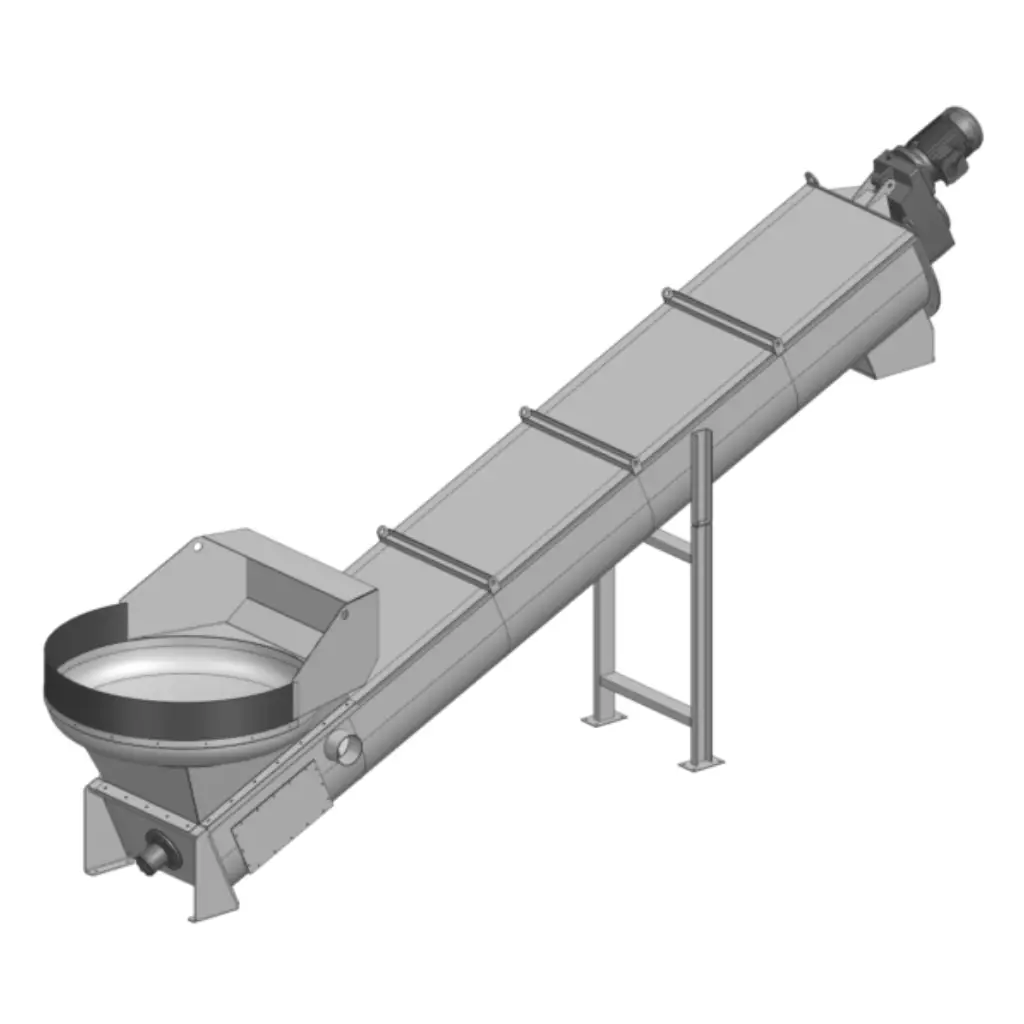
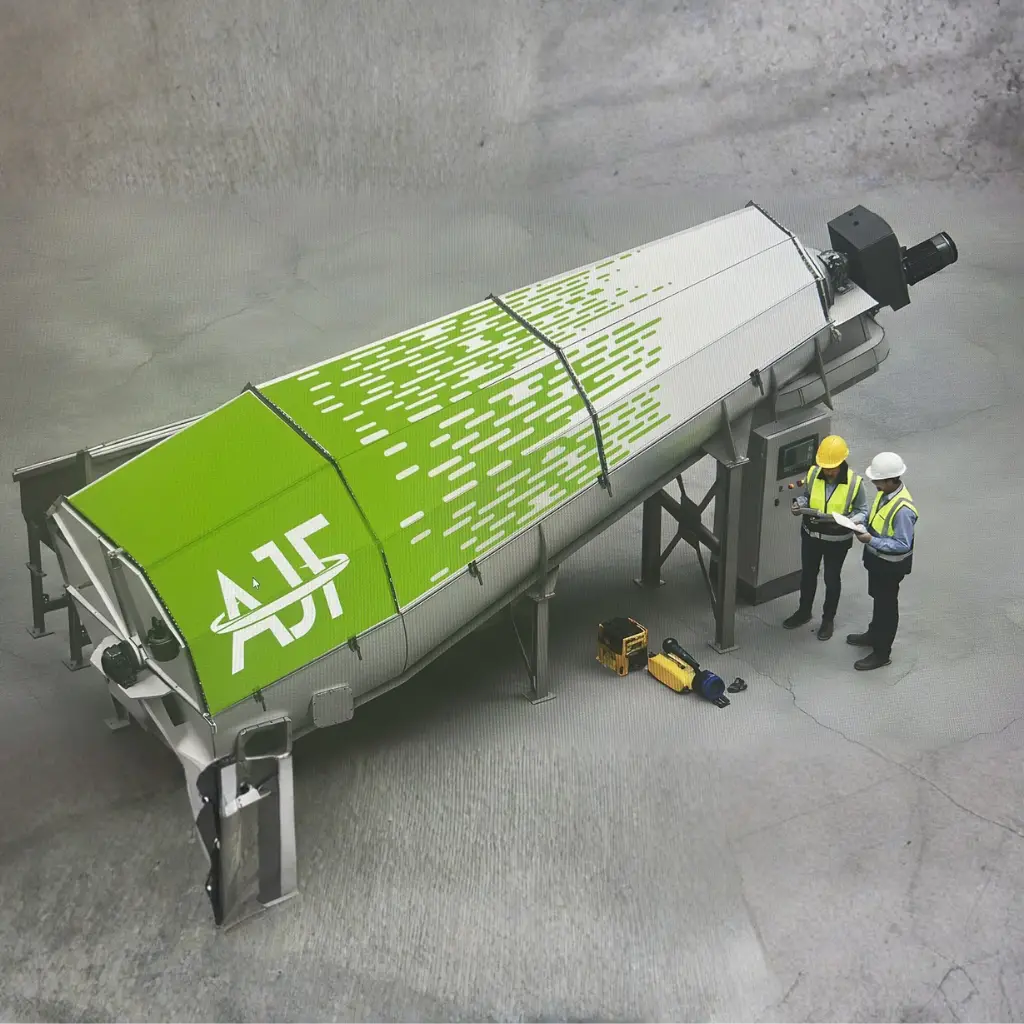
AJF recycling screws are available in two sizes. Here we offer a cost-effective yet highly efficient recycling system for small quantities of return concrete.
Compact and economical design
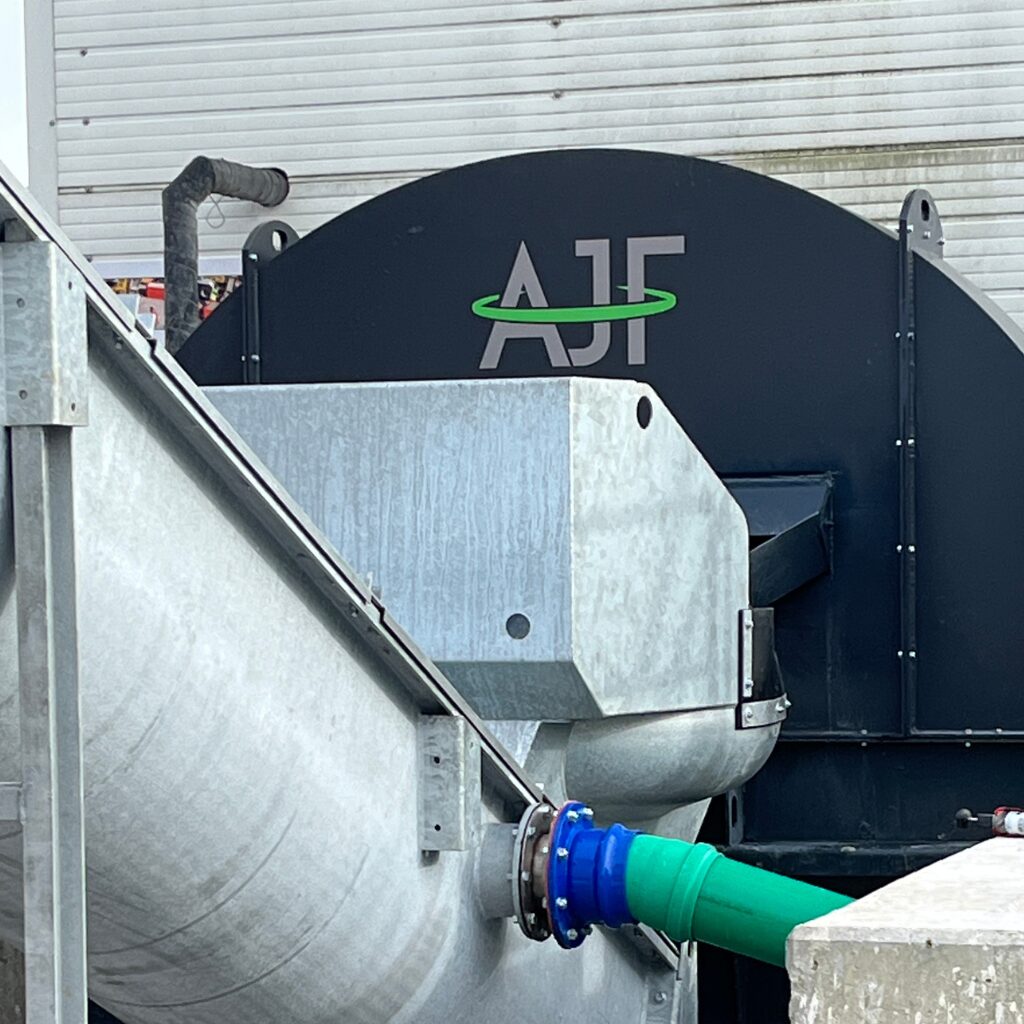
Robust, fully galvanised model with centralised lubrication of the lower worm gear bearing.
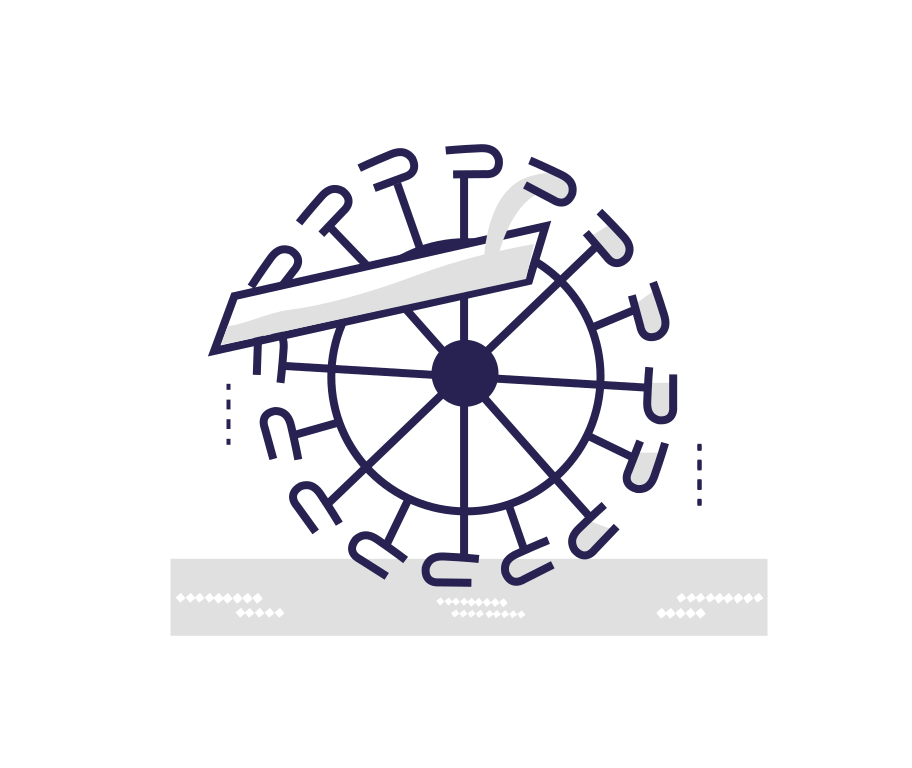
Optional bucket wheel for recovering concrete returning from concrete pumps or wheelbarrows
Thanks to its compact design, the system requires only a small footprint and can be positioned flexibly—ideal even for confined spaces.
Reliable operation even in winter
For year-round use, winter-compatible versions are available on request.
Automatic lubrication and optional heating
The integrated central lubrication system is included in the scope of delivery and reliably supplies the upper and lower worm bearings with different amounts of grease. This significantly increases the service life of the system.
Energy efficient
With a low energy requirement of only 11 kW, the system is cost-effective and
environmentally friendly.
High flexibility – also for concrete pumps
The recycling screw can be combined with a scoop wheel as an option. The scoop wheel conveys fresh concrete from a feed table embedded in the ground into the screw. Concrete applied close to the ground can be easily integrated into the regular washing process, eliminating the need for rotating parts or bearings in the ground.
Low maintenance and durable
The special arrangement of the screw flights at a fixed distance ensures the formation of a protective material bed, which significantly reduces wear and minimizes maintenance. The hot-dip galvanized trough also guarantees a very long service life.
Efficient in operation
The cleverly designed feed hopper allows loading from different directions – even with one or two truck mixers at the same time. Its geometry provides reliable protection against overfilling. Thanks to the increased discharge height, generous material storage is possible. The separation accuracy remains constant at a maximum of 0.25 mm.
Technical details
Technical Specification
Hot-dip galvanised trough
for maximum durability
Hardox HD400 worm gear
for maximum wear resistance
Automatic centralised lubrication
(standard)
Flexible configuration
round hopper or 4 m wide feed table
Optional
integration of a bucket wheel for picking up close to the ground mobile version with stirring tank included heating for winter use
Hot-dip galvanized trough
for maximum durability
Screw conveyor made of Hardox HD400
for maximum wear resistance
Automatic central lubrication
(Serie)
Flexible configuration
Round hopper or 4 m wide infeed table
Optional
Integration of a scoop wheel for ground-level collection
Optional
Mobile version including agitator tank Heating for winter operation
Manufacturers of ready-mixed concrete with up to 8 truck mixers for recycling drum wash water or fresh concrete
precast plants
Closed water cycle for industrial precast concrete production.
Concrete pump operator
For washing out concrete pumps with discharge of fresh concrete close to the ground. In combination with our scoop wheel, no installation in the ground is necessary.
construction sites
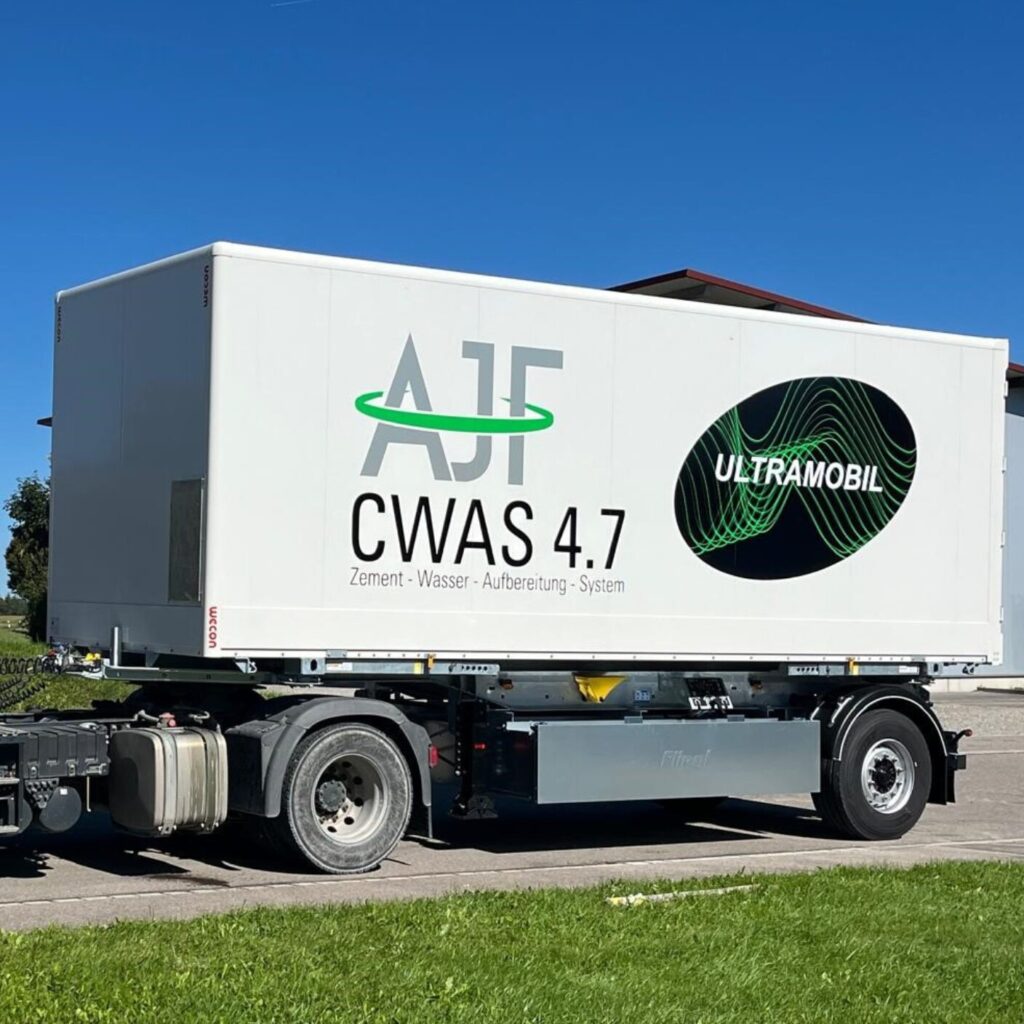
Temporary use on construction sites as a mobile concrete recycling plant
Technical data:
RCS 6
RCS 8
Capacity
12 m³/h
22 m³/h
Electrical power
11 kW
11 kW
Discharge height
2 m
2,15 m
MEASURABLE BENEFITS
Your benefits at a glance
The recycling of fresh concrete affects both precast plants and ready-mix concrete manufacturers. In both cases, excess fresh concrete can be broken down into its components: gravel, sand, and residual concrete water.This process offers your company significant advantages:
Savings on disposal costs
for concrete slurry when using settling tanks
Compliance with legal environmental regulations
through closed-loop recycling
Resource conservation and cost savings
by reusing the washed mixed gravel in concrete production
CO₂ reduction
by eliminating additional transport routes
Ready for your success story?
Then get in touch with us now!
Our experts work with you to develop the optimal solution for your business—cost-effective, sustainable, and future-proof.
With its bucket wheel, AJF offers a powerful, flexible, and cost-effective solution for collecting concrete-water mixtures at ground level. Direct transfer to recycling facilities increases efficiency, reduces waste, and makes logistics more sustainable and profitable.
Maximum material intake directly at floor level
No need for a complex process to lower the recycling plant into the ground
Robust construction and long service life thanks to a galvanized base assembly
The powerful recycling plant with a large water bath. Large quantities of returned concrete, even from several truck mixers at the same time, can be washed out here without any problems.
Large washing capacity with high serviceability
Fully galvanised lower trough for long service life and hinged upper section for easy access
Can be expanded with a density meter to determine the residual water density